

How to prevent and control excessive iron content in aluminum alloy die‑casting production?
Aluminum alloys and zinc‑aluminum alloys are the main raw materials for die‑casting production. Casting quality is affected by multiple factors including raw‑material purity and production processes. Among these factors, iron content control is a critical aspect often overlooked by many die‑casting plants.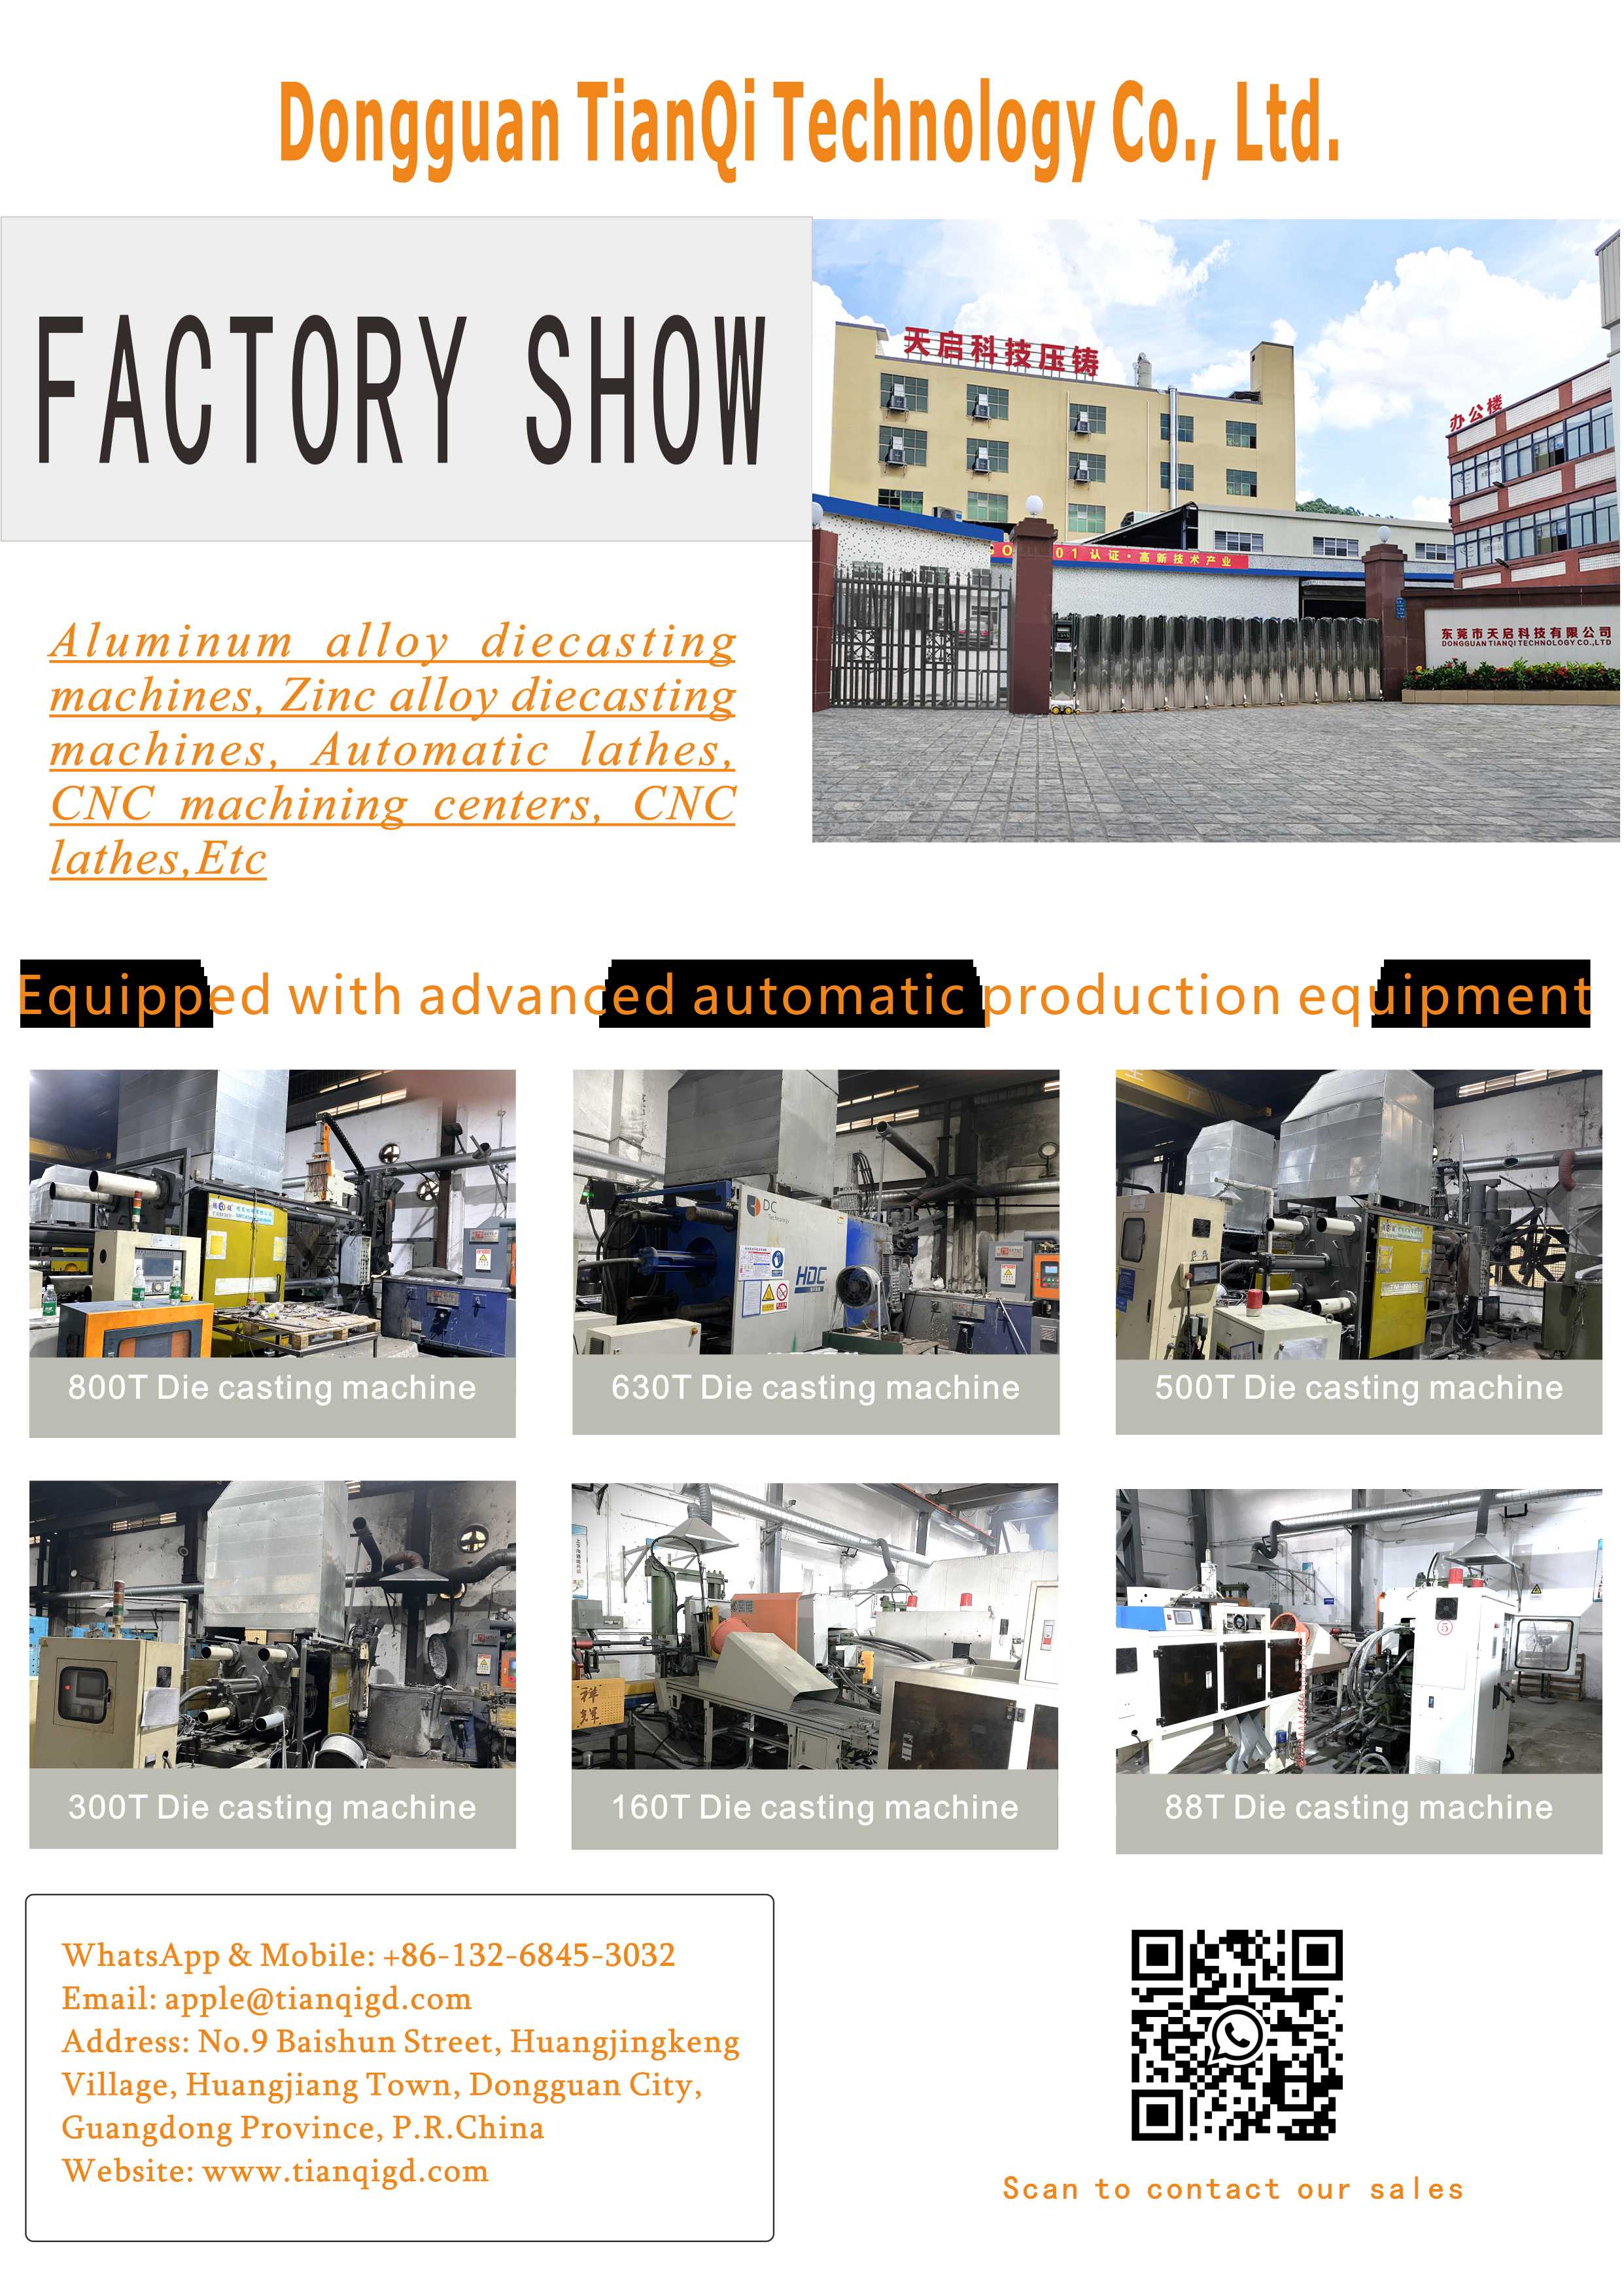
An appropriate iron content can reduce the risk of molten aluminum sticking to moulds and provide certain benefits for die‑casting forming. However, once the iron content exceeds the alloy standard range, acicular brittle microstructures will form inside castings, directly lowering the toughness and strength of castings. Defects such as cracking and brittle fracture are prone to occur, which seriously impair product service performance.
Iron is ubiquitous on production sites. Reliance solely on raw‑material control is insufficient to avoid excessive iron content; full‑process protection measures are required.
First, conduct incoming‑material inspection. Perform spectral analysis on each batch of incoming alloy raw materials. Raw materials with unqualified iron content must not be put into production, so as to avoid excessive iron from virgin materials at the source.
Second, strictly guard against iron dissolution contamination from equipment and tooling. High‑temperature molten aluminum dissolves iron tools. Tooling in contact with molten aluminum, such as crucibles, pouring ladles and stirring implements, shall be applied with protective coatings to prevent bare iron from direct contact with molten aluminum. Meanwhile, avoid over‑heating and prolonged holding of molten aluminum to minimize iron dissolution from ferrous equipment into the molten aluminum.
Returned scrap is also a major source of iron enrichment. Returned materials including gates, flash and rejected castings shall be stored separately to prevent contamination by iron filings and rust. Magnetic separation for iron removal shall be carried out before reuse, and the proportion of returned scrap in use shall be controlled to prevent batch defects caused by large amounts of iron impurities introduced by waste materials.
Finally, implement spot checks during production. Test the composition of molten aluminum after smelting, and proceed with die‑casting only after confirming that iron content is within a reasonable range.
Iron cannot be completely eliminated. Controlling iron within a reasonable range during production can not only realize its anti‑sticking‑to‑mould effect, but also avoid defects induced by acicular crystals, so as to stabilize the overall quality of castings.


